Why Choose a Prototype Machine Shop for Custom Parts?

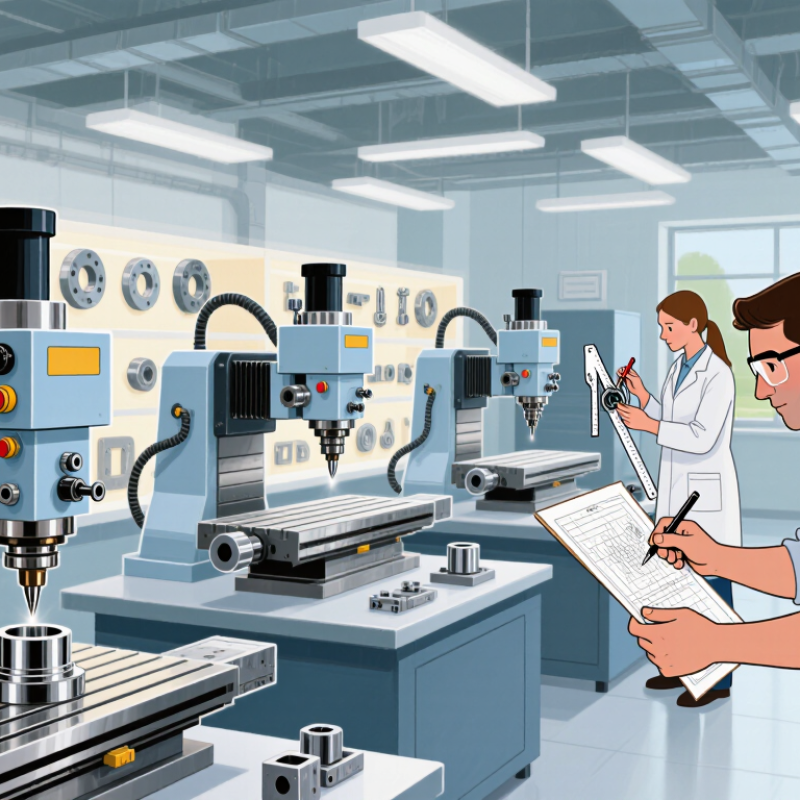
Choosing a prototype machine shop can shape the success of a custom part long before production begins. A capable shop turns digital drawings into physical evidence. It reveals whether a tight tolerance is necessary, practical, or simply inherited from an early concept.

Experienced machinists work with CNC milling, turning, drilling, and finishing processes every day. They understand how aluminum, stainless steel, plastics, and engineering alloys behave under cutting forces. Their advice can prevent warped surfaces, weak walls, and unnecessary machining costs. It should be specific.

A reliable prototype machine shop also supports clear communication. Engineers can review tool access, corner radii, thread depth, and inspection requirements before cutting material. Quality records, dimensional reports, and sample photos create traceability. These details matter when a part must fit beside a sensor, bracket, or moving assembly.

Still, no shop can correct every design mistake. A rushed drawing may hide a conflicting tolerance or an impossible assembly sequence. That is part of the learning process. The best suppliers explain problems without overstating their capabilities. They may suggest a simpler feature, a different material, or one more test iteration.

Prototype work is not only about speed. It is about reducing uncertainty with measurable evidence. When craftsmanship, engineering judgment, and honest feedback meet, custom parts become easier to validate. The right partner does not merely make the component. It helps prove that the component deserves to move forward.
Why Choose a Prototype Machine Shop for Custom Parts?

Prototype Shops Use CNC Tolerances as Tight as ±0.005 in (±0.127 mm)

Why Choose a Prototype Machine Shop for Custom Parts?

Prototype Shops Use CNC Tolerances as Tight as ±0.005 in (±0.127 mm)

A capable prototype machine shop can produce custom parts with CNC tolerances as tight as ±0.005 in (±0.127 mm). This accuracy depends on material, geometry, tool wear, machine condition, and inspection methods. Experienced machinists review the drawing before cutting metal. They check datums, hole locations, wall thickness, and surface finish requirements. A small aluminum bracket may need different controls than a stainless-steel fitting.

In practice, reliable shops measure critical features with calibrated instruments and record the results. They may inspect a first article before producing additional pieces. Temperature also matters. Metal expands slightly during machining, so careless measurement can create avoidable variation. I have seen designs specify extremely tight tolerances where a looser range would work just as well. That mistake increases cost without improving performance. Prototype work helps expose such assumptions early.

Tips: Mark only functional dimensions as critical. Ask how the shop will measure them. Confirm the material and inspection temperature. Keep ±0.005 in for features that truly need it. Too many tight tolerances can slow production and complicate assembly. A useful drawing explains why accuracy matters, not just how much accuracy is requested. The best prototype process combines careful machining, practical engineering judgment, and honest feedback.
CAD-to-Part Workflows Can Reduce Prototype Lead Times to 1–4 Weeks

Why Choose a Prototype Machine Shop for Custom Parts?

CAD-to-Part Workflows Can Reduce Prototype Lead Times to 1–4 Weeks

A prototype machine shop can turn a verified CAD file into a physical part within one to four weeks. The timeline depends on material, tolerance, quantity, and inspection needs. A digital workflow removes repeated drawing transfers and reduces manual quoting errors. Engineers can review toolpaths, fixtures, and critical dimensions before cutting begins. That early review matters when a small bore or thin wall affects assembly.

The National Association of Manufacturers reported that 65.7% of manufacturers faced employee attraction and retention challenges in its 2024 outlook survey. Digital production records can reduce dependence on scarce manual coordination. The World Economic Forum’s Future of Jobs Report 2023 also found that 44% of workers’ skills may be disrupted by 2027. Prototype shops using connected CAD, machining, and inspection processes can respond faster. Still, one to four weeks is not guaranteed. Complex alloys, tight tolerances, or late design changes can extend the schedule. That limitation deserves honest planning.

Tips: Send native CAD files, drawings, material grades, and tolerance notes together. Mark critical surfaces clearly. Request a manufacturability review before approval. Keep one design owner responsible for revisions. A practical mistake is treating a prototype like a production part; the first build should expose weak assumptions, not hide them.

Low-Volume Runs Commonly Range from 1 to 100 Custom Parts

Why Choose a Prototype Machine Shop for Custom Parts?

Low-volume runs commonly range from 1 to 100 custom parts. This range suits teams testing fit, function, and assembly before larger production. A prototype machine shop can adjust toolpaths quickly between small batches. That flexibility matters when a drawing changes after the first inspection.

A capable shop reviews the CAD model, material, tolerances, and intended use before cutting metal. Experienced machinists also identify thin walls, deep pockets, and difficult clamping points early. For example, a tight bore may require a measured finishing pass instead of one aggressive cut. Parts are checked with calibrated tools, including micrometers, gauges, and coordinate measuring equipment when needed.

The first setup is rarely perfect. That is normal. A small run makes correction less expensive. After inspecting the first few parts, the machinist may refine feeds, speeds, or fixture alignment. Clear inspection records help engineers compare dimensions and approve changes with confidence. However, not every prototype needs extreme precision everywhere. Unnecessary tolerances can increase machining time and cost. Thoughtful review is essential. One overlooked detail, such as an unclear edge-break requirement, can still delay delivery. For runs from 1 to 100 parts, direct communication and documented checks often matter as much as cutting speed.

Why Choose a Prototype Machine Shop for Custom Parts? - Low-Volume Runs Commonly Range from 1 to 100 Custom Parts

A practical comparison of prototype machining and conventional high-volume production for custom components.

Decision Dimension Prototype Machine Shop High-Volume Production Approach
Typical Order Quantity 1–100 custom parts is a common low-volume range for prototypes, engineering samples, and pilot builds. Generally intended for much larger quantities where dedicated tooling, fixtures, or automated production can be economically justified.
Primary Objective Validate form, fit, function, assembly, and manufacturability before committing to larger-scale production. Produce repeatable parts at high output with a focus on unit-cost reduction and production efficiency.
Tooling Requirements CNC milling and turning can often produce parts directly from digital CAD data without dedicated production molds or dies. May require substantial upfront tooling, such as injection molds, stamping dies, or specialized fixtures.
Design Flexibility Suitable for frequent design changes because revisions can be made to the CAD program, setup, or machining strategy. Design changes may be more disruptive when dedicated tooling, validated processes, and production inventory are already in place.
Material Options Common choices include aluminum, stainless steel, carbon steel, brass, copper, titanium, engineering plastics, and other machinable materials. Material selection may be optimized around the chosen mass-production process, tooling life, cycle time, and material availability.
Suitable Processes CNC milling, CNC turning, drilling, tapping, surface finishing, deburring, and selected secondary operations are commonly used. May combine molding, casting, stamping, forging, automated machining, or other processes selected for sustained production volume.
Lead-Time Advantage Avoiding dedicated mold or die fabrication can shorten the path from approved CAD data to first physical parts. Initial production may take longer when tooling design, fabrication, sampling, and process validation are required.
Cost Structure Usually has a higher unit price than mass production, but lower upfront investment and less financial exposure for small batches. Often achieves a lower unit cost at scale, but tooling, setup, minimum order quantities, and inventory can increase initial expenditure.
Quality Verification Parts can be inspected against engineering drawings, CAD dimensions, tolerances, surface-finish requirements, and functional criteria. Quality systems typically emphasize process capability, production consistency, statistical monitoring, and inspection across larger lots.
Best-Fit Applications Useful for concept prototypes, functional prototypes, replacement parts, test fixtures, low-volume equipment, and pilot production. Best suited to stable designs with predictable demand and sufficient volume to absorb tooling and process-development costs.
Risk Reduction Allows engineers to discover tolerance, assembly, material, and performance issues before making a larger production commitment. Scaling a design before adequate validation can increase the cost of correcting defects, reworking tooling, or managing excess inventory.
Most Valuable Benefit Speed, flexibility, and controlled investment during the development and validation stages. High throughput and lower per-part cost after the design and production process have become stable.
Note: Actual quantities, lead times, tolerances, materials, and costs depend on part geometry, material, surface finish, inspection requirements, machine capacity, and production schedule.

GD&T per ASME Y14.5 Controls Form, Fit, and Function Requirements

Why Choose a Prototype Machine Shop for Custom Parts?

GD&T, defined by ASME Y14.5, controls more than dimensional accuracy. It connects form, fit, and function through datums, feature controls, and tolerance zones. A prototype machine shop interprets these requirements before cutting metal. Engineers review datum schemes, material behavior, inspection access, and assembly conditions. A flatness callout may look simple. It can become difficult after machining stress is released.

According to a 2023 global smart-manufacturing survey, 86% of manufacturers expect smart manufacturing to drive competitiveness within five years.

That shift increases the value of traceable digital inspection. Prototype teams can link CAD models, GD&T callouts, coordinate-measuring-machine results, and revision records. The result is clearer evidence that a part meets its functional intent. Small details matter. A misplaced datum can control the wrong surface. A profile tolerance can reveal a problem that linear dimensions miss.

In practical shop work, machinists often identify unclear tolerances before production begins. They may ask whether a hole pattern controls assembly alignment or only location. That conversation prevents expensive rework. Yet GD&T is not magic. A perfect drawing can still contain an unrealistic tolerance stack. I have seen designs become harder to inspect than to manufacture. Early feedback helps, although it may challenge the original design. ASME Y14.5 remains the technical foundation, while inspection planning turns its language into measurable proof.

Material, Inspection, and Certification Data Guide Shop Selection

Why Choose a Prototype Machine Shop for Custom Parts?

Material, Inspection, and Certification Data Guide Shop Selection

Choosing a prototype machine shop involves more than checking its equipment list. Material control often reveals the shop’s real discipline. Ask how stock is identified, stored, and matched to each work order. For stainless steel, aluminum, or engineering plastics, request material certificates before cutting begins. Heat numbers, grade, temper, and lot details should remain traceable. A clean certificate is useful, but it is not proof by itself. Storage labels and receiving records matter too. I have seen good parts delayed because a certificate referenced the wrong lot. Traceability matters.

Inspection capability should match the part’s risk, not merely its size. Confirm which features are measured, with what tools, and at what stage. Coordinate measuring machines help with complex geometry, while calibrated gauges suit simple dimensions. Ask for inspection reports showing actual values, tolerances, and equipment status. Photos of fixturing can add useful context. Do not accept a generic statement such as “fully inspected.” It sounds reassuring, but it leaves too many questions. One practical weakness deserves attention: prototype schedules can encourage rushed checks. Build inspection time into the quotation and review plan. That gap is costly.

Certification data should support the manufacturing story, not decorate a folder. Request certificates of conformance, material reports, calibration records, and approved drawing revisions. Check whether each document names the part number, revision, quantity, and inspection status. Secure file naming makes later audits faster. It also prevents confusion when several prototypes look nearly identical. Ask who approves nonconforming material and how changes are recorded. A capable shop should explain this without hesitation. Still, explanations can be incomplete. I prefer a sample report over a polished promise. It shows measurement dates, signatures, methods, and deviations.

Warning!

You are using an outdated browser. Things may not appear as intended. We recommend updating your browser to the latest version.

Close