Top 10 Die Cast Part Surface Finishing Options
Choosing a finish for a die-cast component is not just a cosmetic decision. Die Cast Part Surface Finishing can affect corrosion resistance, wear, cleanability, and how reliably a part fits with neighboring components. The right process depends on the alloy, the part’s geometry, its working environment, and the appearance customers expect.
A casting may come from the mold with parting lines, gate marks, or small surface pores. These details matter. A coating can make a surface look uniform, but it may also reveal defects or build up around edges and holes. Some processes remove material; others add a layer. Check critical dimensions after finishing, especially where threads, seals, or close-fitting interfaces are involved.
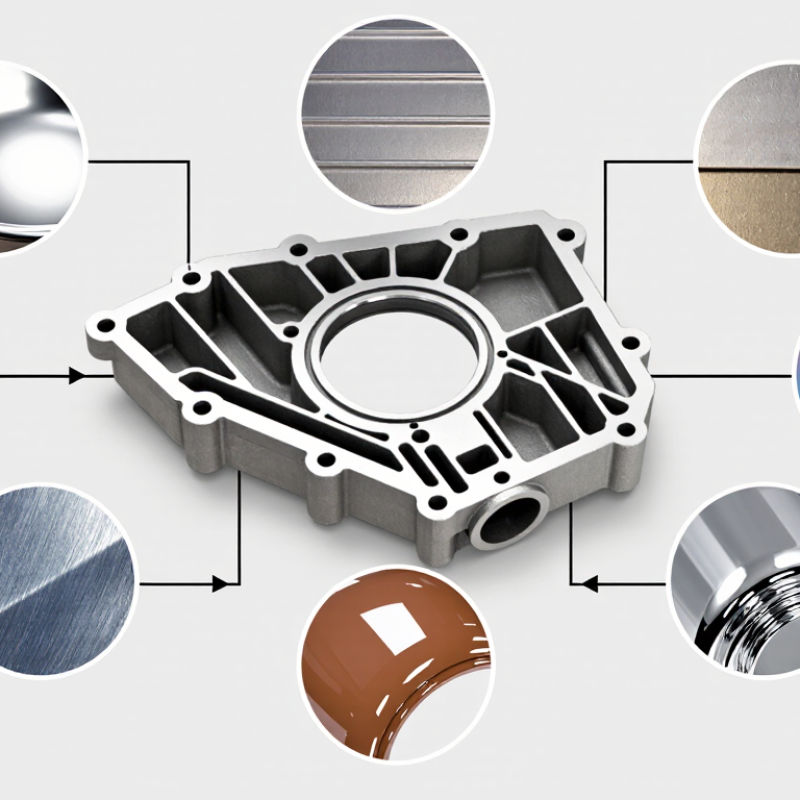
The options in this guide range from mechanical methods, such as polishing and abrasive blasting, to treatments such as painting, powder coating, and plating. Each has trade-offs in cost, appearance, durability, and process control. Aluminum alloys, for example, do not always respond identically to the same treatment, so confirm compatibility with the material supplier or finishing provider. A test sample helps.
There is no universal best finish. A glossy surface may look impressive under showroom lights and still be wrong for a part exposed to abrasion. The comparisons below explain what each option can do, where it may fall short, and which practical questions to ask before specifying it. Even experienced teams sometimes choose by habit. That deserves a second look.
How Alloy Chemistry, Porosity, and Silicon Content Affect Die-Cast Finishes
Top 10 Die Cast Part Surface Finishing Options
A finish can look excellent on one casting and uneven on another. Alloy chemistry helps explain why. In aluminum alloys, silicon improves flow into thin ribs and complex cavities. It can also leave silicon-rich areas that respond differently to polishing, etching, or anodizing. Small details matter. A decorative anodized surface may show color variation, while paint or powder coating can provide more consistent coverage. The best choice depends on appearance, service conditions, and the casting’s actual surface.
Porosity creates another challenge. Tiny pores near the surface may hold air or process fluids, then cause blisters during plating or when a coated part is heated. Impregnation, careful cleaning, and controlled coating thickness can reduce risk, but none repairs every casting defect. Inspecting sample parts before committing to a finish is practical. It also catches surprises early.
For bright finishes, polishing or plating can highlight pits and flow marks rather than hide them. Conversion coatings and paint are often more forgiving, though they still need clean, well-prepared metal. High-silicon aluminum may require trials before a specific anodizing color is approved. I would not treat this as a fixed recipe. A small test batch can reveal whether the chosen alloy, pore structure, and finish work together. The first sample may still need adjustment.
Compare 10 Finishes by Film Build: Powder Coating Typically Measures 50–100 μm
Film build matters on die cast parts because coating thickness can change fit as well as appearance. Powder coating typically measures 50–100 μm after curing, depending on the powder and application process. That is a substantial layer. It can cover minor surface texture, but may soften crisp edges or narrow a threaded hole. A 75 μm coating on both sides of a close-fitting feature can affect assembly clearance.
When comparing ten finishing options, separate processes that add material from those that do not. Liquid paint, plating, and anodizing add a film, but their thickness varies by specification and process. Polishing and blasting change the surface without adding a coating layer; conversion coatings are generally much thinner. Powder coating’s 50–100 μm range is useful for early design checks, not a guaranteed production value. In practice, the number is not perfectly tidy.
Check thickness on representative castings, including edges and recessed areas, because coverage can vary across a complex shape. Die castings may also release trapped gas during curing, leaving small pinholes in the finish. A test run can reveal this before production quantities are committed. I would confirm the measurement method and tolerance with the finishing supplier, then check critical fits on coated parts.
Top 10 Die Cast Part Surface Finishing Options
Typical coating film build by finish (μm)
Bars show indicative minimum-to-maximum film-build ranges. Powder coating typically measures 50–100 μm. Actual build depends on the substrate, part geometry, specification, and process; conversion coatings are much thinner than paint or plated finishes.
Evaluate Coating Adhesion with ASTM D3359’s 0B–5B Rating Scale
A glossy die-cast housing can look flawless and still lose its coating at a sharp edge. ASTM D3359-23 provides a practical tape-test scale for checking adhesion on metal surfaces.
In Method B:
5B means no coating squares detach
4B indicates less than 5% removal
3B is 5–15%
2B is 15–35%
1B is 35–65%
0B is over 65%
Ratings then decline as removal increases. Method A uses an X-cut and has separate rating criteria, so do not mix the two scales. These results help compare finishes, including paint, powder coating, and conversion coatings. They do not predict service life.
Tips: Test representative parts, not only smooth witness panels. Keep the blade, cut spacing, tape, and removal technique consistent. Record the alloy, surface preparation, coating thickness, and test location. A rough edge or porous casting can change the result. Small details matter.
ASTM D3359 is a comparative test, not a complete measure of durability under heat, moisture, or impact. A 5B result is encouraging, but it does not prove long-term performance. That limitation is easy to overlook. If coatings fail near parting lines or recessed corners, inspect those areas separately and review cleaning and pretreatment controls. A neat score cannot explain every failure.
Interpret ASTM B117 Salt-Spray Hours as Test Results, Not Service-Life Data
A die-cast part may use powder coating, wet paint, conversion coating, plating, or an anodic finish where the alloy permits. Choice depends on alloy, shape, and exposure. An ASTM B117 rating of 500 hours is a test result, not a promise of five outdoor years. The chamber uses controlled salt fog. It does not reproduce sunlight, temperature swings, abrasion, trapped moisture, or actual handling. That distinction matters.
A useful report identifies specimen preparation, coating thickness, scribe condition, and failure criteria. For example, corrosion may creep from a cut edge while the broad coated face still looks sound. Compare like with like: the same alloy, pretreatment, finish, and evaluation rules. Salt-spray hours can help screen finishes or reveal process variation, but they cannot rank every option for every location. A coastal bracket and an indoor control cover face different exposures.
Ask for the actual test report, including whether samples were scribed and how corrosion was scored. Then relate the result to field conditions and maintenance expectations. I would not convert hours into service years. It is tempting, but that calculation suggests certainty the test cannot provide. Edges, threaded holes, and casting pores also deserve attention; they can complicate results.
Select a Finish by Corrosion Resistance, Wear, Appearance, and Cost
Die-cast finishes should be selected for the part’s environment, contact points, appearance, and budget. A component exposed to road spray may need paint, powder coating, or a conversion coating, with careful edge coverage. For repeated sliding contact, plating or a suitable wear-resistant coating may perform better. Bright nickel or chrome plating can create a polished look, but added preparation and masking affect cost. There is no universal winner.
Tips: Ask for samples made from the same alloy and with similar surface texture. Check coating thickness around ribs, holes, and sharp edges. Test first. Anodizing can be inconsistent on some aluminum die-cast alloys, so confirm the result with the actual material and supplier process.
For lower-cost cosmetic parts, bead blasting followed by paint can hide minor texture, though scuffs may reveal the substrate. Powder coating gives a thicker film, but tight fits may need masking. Conversion coatings add little thickness and can support paint adhesion, but usually offer limited standalone protection in harsh conditions. Compare corrosion, wear, color consistency, and rework—not just the quoted finish price. A small test panel helps; it still may not predict every production variation.